Confirm dry polymer fits the equipment
Dry friction-reducer powder can be attractive where concentrated polymer supply and lower transported carrier mass suit the operation. Those advantages are conditional on effective feeding, wetting, hydration and transfer. A low powder price cannot compensate for insufficient preparation capacity or repeated plugging at the required pumping rate.
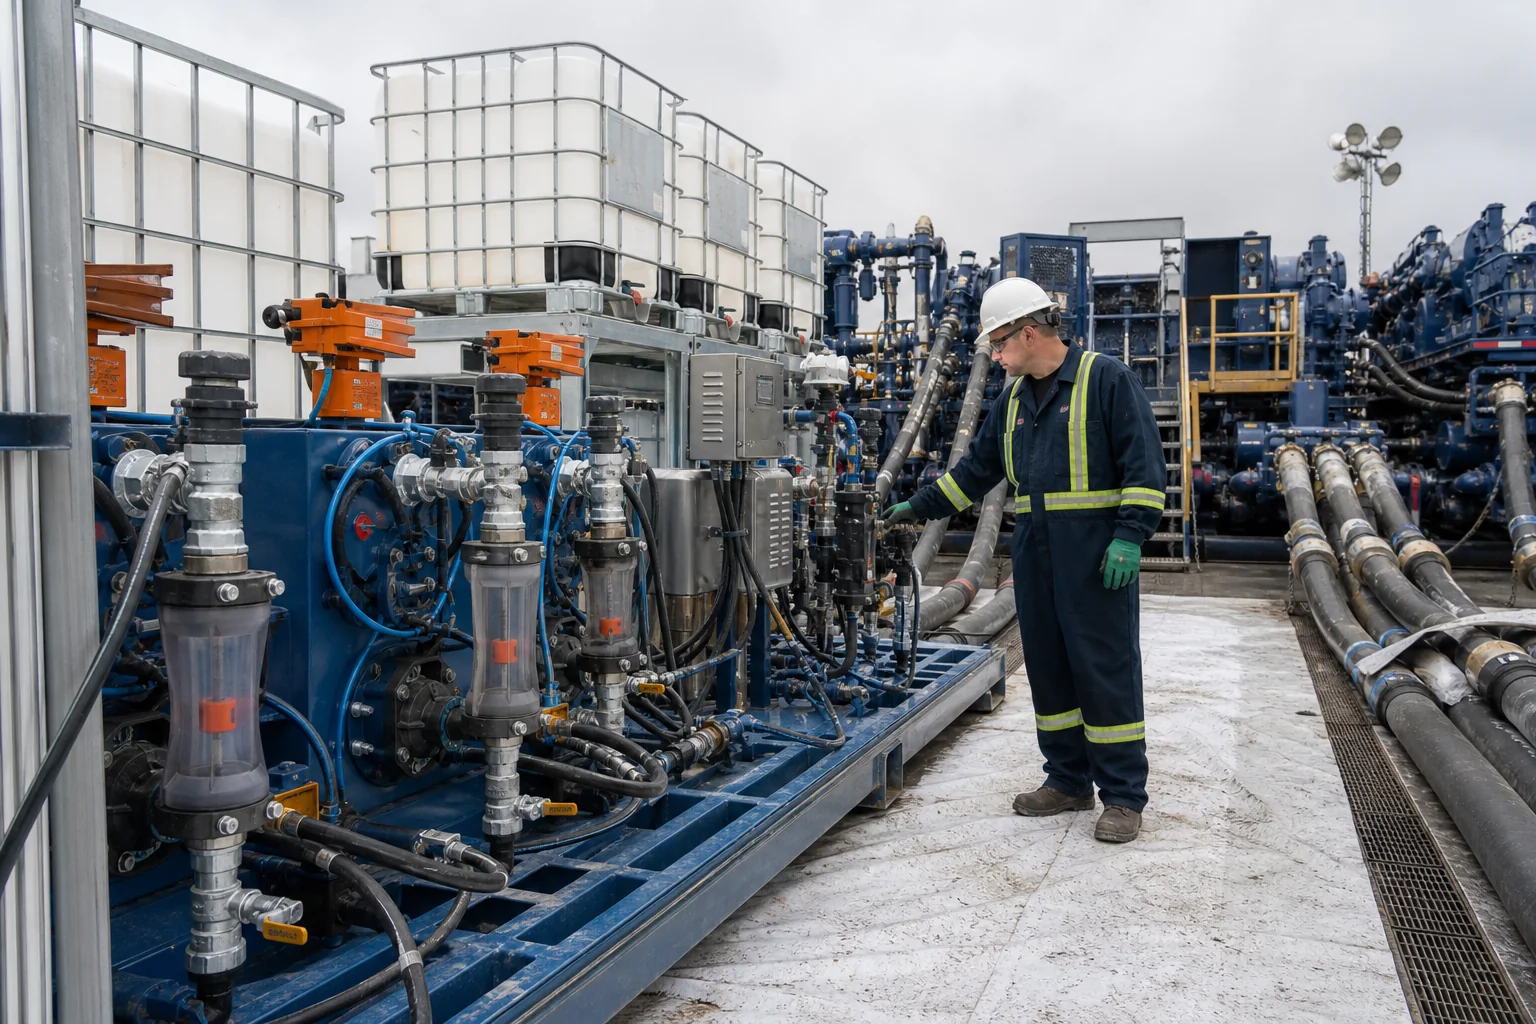
Review the dry friction-reducer duty against the installed unit before requesting a large quantity. Identify whether the proposal needs new equipment, a revised stock concentration or additional residence capacity rather than treating powder as a direct replacement for emulsion.
Describe particle handling and wetting
Request the particle-size information and powder handling guidance relevant to the feeder and wetting system. Evaluate bridging, dust control and feed consistency using representative material. A powder that disperses gently in a small beaker may behave differently through a production hopper under humidity or vibration.
Inspect wetting for agglomerates and undispersed particles without assuming a clear-looking solution is fully hydrated. Record water rate, powder rate, mixing energy and observation time. Do not use an improvised high-shear treatment to conceal poor wetting while introducing another source of polymer damage.
Match hydration capacity to throughput
Calculate actual available residence from useful preparation volume and solution withdrawal rate, then consider short-circuiting and operating interruptions. Supplier hydration instructions are a starting point for a verified site procedure. Include the lowest expected water temperature and the actual water analysis in the test plan.
The hydration-time guide helps distinguish incomplete development from a weak grade. Record solution age at injection and the earliest acceptable pressure response. A fully aged laboratory stock does not prove suitability for an on-the-fly application.
Specify tests that follow the powder into service
Use the same powder identity, feeder and preparation procedure for the loop evaluation and field trial. Record screen residue or undissolved material using a defined sampling method where these checks matter. Compare pressure response after the representative transfer path, not only immediately after gentle laboratory mixing.
Request the analytical basis behind dry matter, active polymer and any viscosity specification. Moisture, total solids and polymer activity are not interchangeable measurements. Set justified receiving limits with the supplier rather than copying an arbitrary high molecular-weight statement into the order.
Protect bags and receiving operations
State bag size, liner, pallet, wrapping and unloading requirements. Dry storage and damaged-package quarantine should be planned before delivery. Moisture exposure can alter feeding and make-down behaviour even if the nominal chemical identity remains unchanged.
Check whether the site can segregate lots and protect opened bags between shifts. Match stock rotation to actual demand and the grade's written storage guidance. The bag and container checklist gives packaging questions without claiming a standard pack or universal storage life.
Compare the complete purchase
Include preparation water, labour, equipment, energy, waste and verified consumption in the commercial comparison. Compare on the same treated-water duty and approved active basis where appropriate. Do not assume powder must outperform emulsion simply because its transported active fraction may be higher.
Send feeder details, tank volumes, water temperature, target rate and planned trial quantity through the dry friction-reducer buying enquiry. Request coded samples and a feasible preparation procedure before asking for a bulk commitment tied to a schedule the equipment cannot support.